
Condensate Management
Mechanical Float Drain
Condensate drained by the liquid itself: no power, nothing to set, and no compressed air lost.
Product overview
A drain that runs on buoyancy
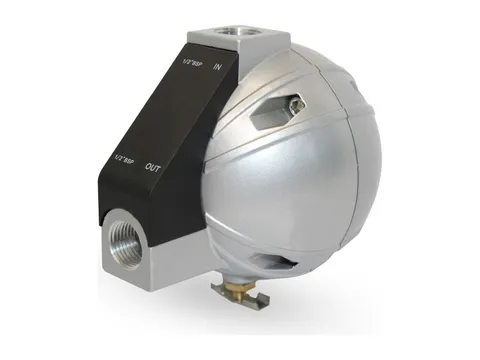
Our mechanical float drain uses the buoyancy of a float to drain condensate from your compressed air equipment. As liquid collects in its small chamber it lifts the float, and the float opens the discharge valve. As the level falls, the float drops and closes the valve before the liquid uncovers the seat.
The seat always sits under a column of liquid, so condensate leaves and compressed air stays in your system. The only gas lost is the air dissolved in the condensate, about 0.15 litres of free air per litre at 7 bar g and 20 °C.
It needs no electrical supply, cabling or signal connection: the liquid provides the actuating force and system pressure the discharge force. That makes it a natural fit for hazardous areas, outdoor pipe racks, mobile compressors, remote drip legs and filter housings.
- About 0.15 LFree air lost per litre of condensate
- About 250 L/hThrough a 2 mm orifice at 7 bar g
- More than 10 ×The aftercooler load in hot, humid conditions
- ZeroPower supply or cabling needed
Benefits
The problems it solves
Condensate forms around the clock, often far from a power supply. Here is what goes wrong at drain points, and how the float drain deals with it.
-
Air lost at drains
The problem
A 3 mm orifice left open at 7 bar g passes roughly 30–40 m³/h of free air, around 30,000 kWh a year from a single drain stuck open.
How it solves it
The water seal above the seat keeps air in your system, and only dissolved air leaves with the condensate.
-
No power at the drain point
The problem
Drip legs on outdoor mains, receivers on roofs and filters inside machines often have no electrical supply, and cabling dozens of points is costly.
How it solves it
The drain needs no cabling at all, and keeps working through power failures.
-
Hazardous zones
The problem
In ATEX and IECEx zones, electrical equipment needs certification.
How it solves it
With no electrical ignition source, float drains are fitted in ATEX and IECEx zones.
-
Loads that swing
The problem
Condensate load swings from a humid afternoon to a dry night or a shutdown.
How it solves it
Opening and closing levels are fixed by the float geometry, so the drain follows the load in summer and winter alike and cannot be mis-adjusted.
-
Flooded dryers and filters
The problem
A liquid slug entering a dryer exceeds its moisture capacity and raises the outlet dew point, and coalescing elements standing in liquid pass oil and water downstream.
How it solves it
Continuous drainage keeps slugs and flooded bowls away from your downstream treatment stages.
-
Corroded receivers
The problem
Water standing on the base of a steel vessel corrodes the shell.
How it solves it
Your receivers stay free of standing water.
Where it’s used
Wherever power is hard to reach
Float drains serve every collection point in a compressed air system, and come into their own where running a power supply is impractical.
-
Oil, gas and petrochemicals
Non-electric drains on instrument air separators and drip legs inside ATEX and IECEx hazardous zones.
-
Power generation
Instrument and service air systems, including receivers outdoors on plant structures.
-
Food and beverage
Drains on the coalescing filters that achieve the BCAS Guideline 102 classes for food-contact air.
-
Pharmaceuticals and healthcare
Filter housings and receivers of production air and medical air plant.
-
Automotive and surface finishing
Drip legs ahead of paint booths and blast rooms, before water reaches spray guns and blast nozzles.
-
Textiles
Air-jet looms and spinning machines in humid halls, with heavy condensate loads in the network.
Also general manufacturing and engineering, mining, tunnelling and construction, rail and transport, water and wastewater treatment, plastics and packaging, and filter bowls in workshops and small plants.
How it works
Float, open, reseal
The liquid does the sensing and your system pressure does the pushing. No power, no timer, no settings.
-
1. CollectCondensate runs into the chamber by gravity, and the air it displaces returns through the inlet or balance line. The float rests low and the valve is shut.
-
2. RiseAs the level climbs, the float's buoyancy grows. At 7 bar g, pressure holds the plug on a 2 mm seat with about 2.2 N.
-
3. OpenThe float's lift, multiplied by the lever, exceeds the pressure force on the seat and the valve opens, with no electrical supply.
-
4. DischargeSystem pressure drives the condensate out. At 7 bar g a 2 mm orifice passes about 250 litres an hour.
-
5. ResealThe level falls, the float drops and the valve reseats while liquid still covers the orifice. Only air dissolved in the condensate is lost: about 0.15 litres of free air per litre.
Figures at 7 bar g, for a direct-acting drain with a 2 mm seat.
Get the full details
Our brochure covers it in detail, and our questionnaire tells us what we need to recommend the right one for your plant.
Keep exploring
More from our range
Equipment for every stage of your compressed air, and our own engineers to test, commission and look after it.
-
Refrigerated Air Dryers
Dry, condensate-free air for your plant, with no compressed air spent drying.
View product -
Heated Desiccant Dryers
Deep, stable dew points for your air, with heat doing the regeneration.
View product -
Heatless Desiccant Dryers
Deep dew points without heaters, for hazardous areas and remote sites.
View product -
Breathing Air Systems
Your plant’s compressed air, made safe to breathe.
View product -
Hydrogen Dryers & De-Oxo Units
Electrolytic hydrogen purified of oxygen and water, ready for fuel cells.
View product -
Biogas & Natural Gas Dryers
Dry, condensate-free fuel gas for your engines, boilers and upgrading plant.
View product -
CO₂ Dryers
Beverage-grade dry CO₂ for your recovery plant, with no gas vented.
View product -
Membrane Dryers
Dry air at the point of use, with no power and no moving parts.
View product
-
Coalescing Filters
Takes oil and water aerosols out of your air, down to 0.01 mg/m³.
View product -
Particulate Filters
Dry, dust-free air for your plant, down to 0.01 µm particles.
View product -
Compressed Air Duplex Filters
Change filter elements without interrupting your air supply.
View product -
High Pressure Filters
Certified air purity for your high-pressure lines, up to 350 bar g.
View product -
High Temperature Filters
Particle-free compressed air and gas where your process runs hot.
View product -
Ammonia and Refrigerant Filters
Keeps compressor oil out of your condensers and evaporators.
View product -
Oxygen Filters
Particle-free oxygen for your system, without adding an ignition source.
View product -
Silicone-Free Filters
Crater-free paint finishes, from air free of paint-wetting contaminants.
View product -
Medical Vacuum Filters
Keeps pathogens from hospital suction away from your pumps and exhaust.
View product -
Hydrogen Filters
Particle, aerosol and oil-free hydrogen, from electrolyser to dispenser.
View product -
CNG Filters
Oil-free, particle-free natural gas from your compressor to the vehicle.
View product
-
Centrifugal Moisture Separators
Bulk liquid out of your air by centrifugal force, with no element to replace.
View product -
Oil Water Separator
Turns oily compressor condensate into water fit for sewer discharge.
View product -
Zero-Loss Electronic Drain
Discharges every drop of condensate from your system, never your compressed air.
View product -
Timer Drain
Scheduled, positive condensate discharge from any collection point in your system.
View product -
Vacuum Drain
Empties liquid from your vacuum system without breaking the vacuum.
View product
-
Crane Air Conditioner
Cool, clean cabins and electrical rooms for cranes working in extreme heat.
View product -
Tent Air Conditioner
Controlled climate for your tents, shelters and temporary structures.
View product -
Panel Air Conditioner
Cool, clean, dry control panels, even in your hottest, dirtiest plant areas.
View product -
Air / Water Cooled Air Conditioner
Stable room temperatures for your electrical rooms in extreme plant heat.
View product
-
Hot Tapping
Add measurement ports to your live air lines without stopping production.
View product -
Compressed Air Quality Measurement
Prove your air's ISO 8573-1 purity: particles, oil and dew point.
View product -
Digital Thickness Meter
Measure the metal left in your receivers and pipework, from the outside.
View product -
Dew Point Meter
Proof your air is dry, measured at line pressure.
View product -
Flow Meter
True standard flow of your compressed air, whatever the line pressure.
View product -
Leak Detector
Hear, locate and cost every compressed air leak in your plant.
View product -
Pressure Sensor
Live pressure data from your compressor room to every point of use.
View product -
Humidity Meter
Humidity, temperature and dew point from one probe.
View product -
Power Meter
Measure the true power, energy and efficiency of your compressors.
View product
-
Health Testing of Compressed Air & Gas Dryers
Measured proof your dryer delivers its rated dew point.
View service -
Commissioning and Service of Compressed Air & Gas Dryers
Verified dew point from first start-up through your dryer's service life.
View service -
Compressed Air Quality Testing
Measured, documented proof of your compressed air purity class.
View service -
Dew Point Measurement Testing
Verified pressure dew point at the points that matter in your network.
View service -
Compressed Air Flow Testing
Measured air demand, leakage and cost for your plant, not estimates.
View service -
Wall Thickness Testing
Know the remaining wall, corrosion rate and safe life of your equipment.
View service -
Sourcing
Spares, consumables and whole systems for your plant, sourced globally.
View service
